How to Inspect Custom Drawstring Bags Before Shipment
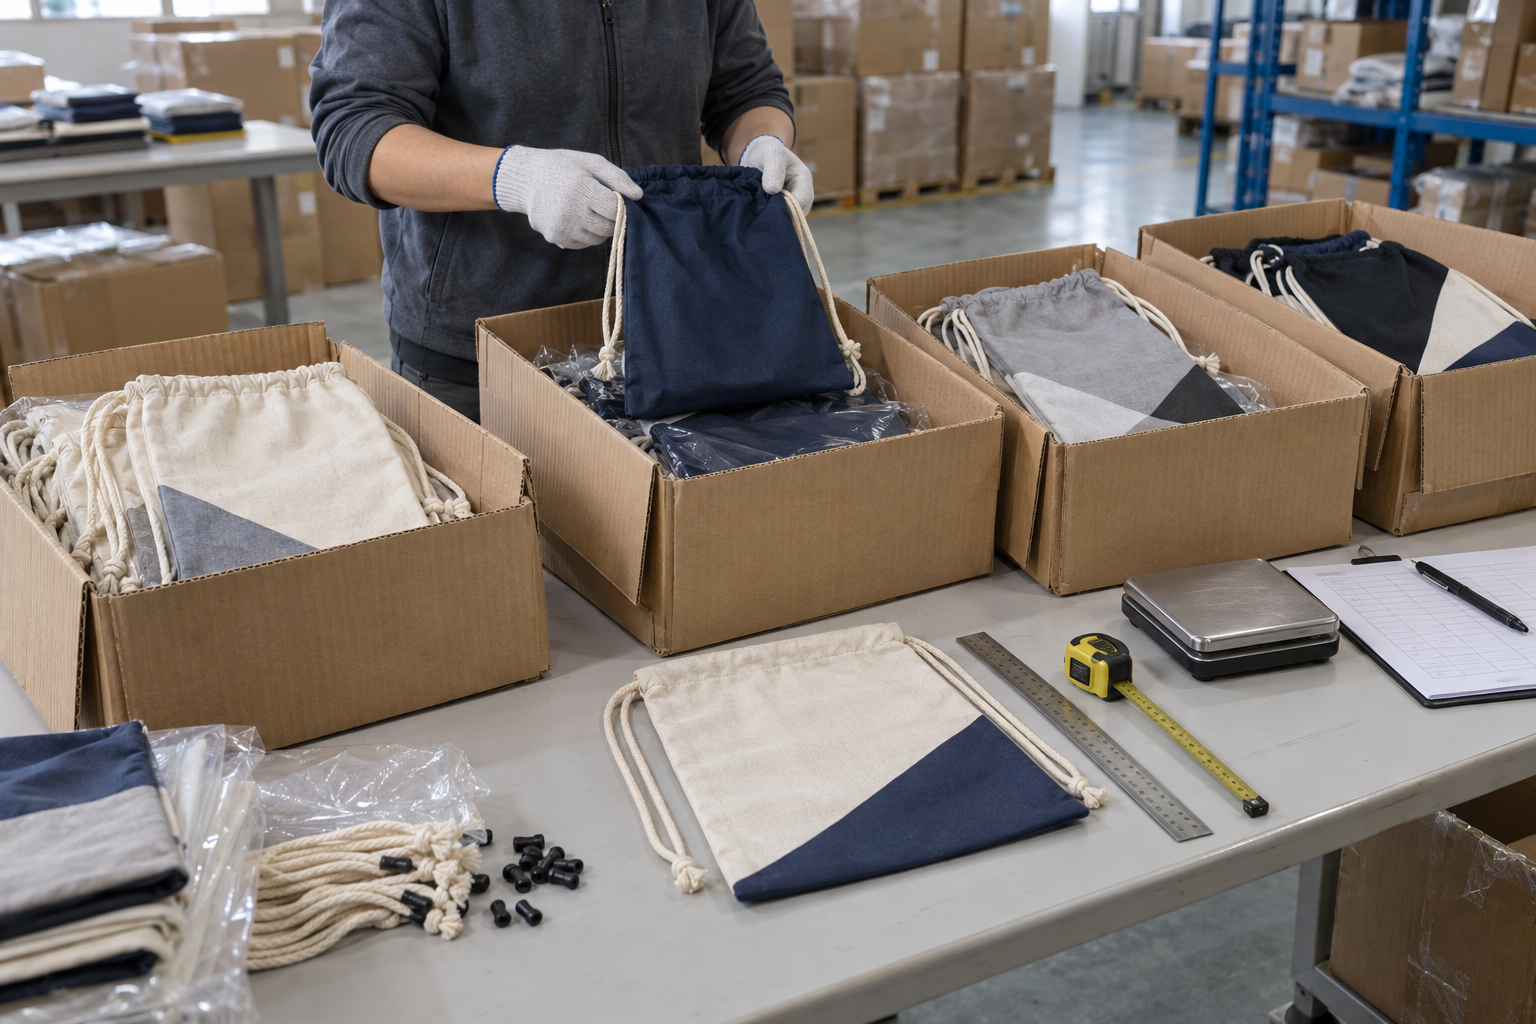
Editorial visualization of final random inspection for generic, unbranded drawstring bags. It is not a documented customer order, factory-ownership claim, third-party inspection, or LUCKYSTAR shipment result.
The short answer: inspect custom drawstring bags before shipment only after the order specification, approved sample, packing requirements and sampling plan are frozen. Confirm the inspection lot, select cartons and units without supplier cherry-picking, check quantity and packaging, then evaluate workmanship, dimensions, material, color, print, cords, reinforcements and agreed functional tests. Record every defect against a pre-agreed critical/major/minor definition, apply the selected sampling standard correctly, and release the shipment only through the authorized disposition process.
A final inspection is a decision gate, not a substitute for production control. It can reveal whether the completed lot appears to meet the written purchase requirements, but a sample cannot prove that every bag is perfect. Buyers sourcing custom drawstring bags should therefore connect the final inspection to approved references, in-process records, order-specific testing and a clear correction/reinspection rule.
What Is a Pre-Shipment Inspection for Drawstring Bags?
A pre-shipment inspection, often called final random inspection, examines a defined finished lot shortly before release. Its purpose is to provide evidence for an accept, reject, hold, rework or conditional-disposition decision.
| Inspection activity | Main question | Appropriate timing |
|---|---|---|
| Incoming material check | Are fabric, cords, eyelets, labels and packing materials correct? | Before cutting or assembly |
| First-article approval | Do construction, dimensions and branding match the approved specification? | At production setup |
| In-process inspection | Is the process remaining controlled while defects can still be corrected efficiently? | During printing, sewing and packing |
| Final/pre-shipment inspection | Does the completed, identifiable lot meet the agreed release criteria? | After production and sufficient packing are complete |
| Loading supervision | Are approved cartons counted, containerized and sealed as instructed? | During dispatch |
The Custom Drawstring Bag Quality Control Checklist covers the full quality chain. This article narrows the scope to the final release gate: what must be ready, how samples are selected, which checks belong in the report and what happens when the result is not acceptable.
Do Not Start Until the Inspection Readiness Gate Is Met
An inspection performed too early can create a misleading result. The buyer and supplier should agree on readiness conditions in the purchase order or inspection instruction.
| Readiness item | Evidence to confirm | Risk if missing |
|---|---|---|
| Production status | Quantity completed, quantity packed and balance status | Samples may not represent the final lot |
| Lot identity | PO, SKU, color, size, artwork version and production/packing lot | Results can be applied to the wrong goods |
| Packing status | Final retail packing and representative export cartons available | Carton, label and pack-out errors remain hidden |
| Approved reference | Signed sample, sealed sample or controlled approval images/specification | Inspector has no objective comparison basis |
| Inspection instruction | Sampling method, defect definitions, tests and report format | Decisions become improvised on site |
| Measuring/test equipment | Suitable equipment with required verification or calibration status | Results may not be reliable |
| Corrective-action access | Authority to open cartons, isolate defects and stop release | Inspection cannot control shipment disposition |
There is no universal percentage of packed goods that automatically makes every order ready. The required production and packing completion status should be written into the inspection booking. If unfinished goods, replacement units or mixed lots can enter after the sample is drawn, the inspected population and the shipped population are not the same.
Build the Inspector’s Reference Pack
The inspection pack is the control center of the final check. It should resolve conflicts before the inspector starts counting defects.
Commercial and product identification
- purchase order and current revision;
- supplier/manufacturer and shipment destination;
- item/SKU, variant, quantity and carton plan;
- material composition or agreed material description;
- color, size and bag construction;
- delivery, labeling and documentation requirements.
Product specification
- dimension sequence and measurement method;
- tolerances and measurement points;
- seam, stitch, drawcord, eyelet or fabric-corner reinforcement details;
- print/embroidery artwork, size, position and color target;
- accessories, pockets, zippers, lining or bottom/gusset details;
- unit packing, assortment, carton, barcode and shipping-mark requirements.
Approval and quality references
- golden sample or pre-production sample;
- approved fabric, cord and color references where applicable;
- defect classification list with photographs if possible;
- sampling standard, edition, inspection severity/level and acceptance criteria;
- functional or destructive test instructions;
- change approvals and concession records.
The drawstring bag tech pack guide explains how to capture these product fields before production. The final inspector should not be asked to resolve a missing specification through personal judgment.
Define the Inspection Lot Before Sampling
A lot is the population from which the sample is selected and to which the decision applies. It must be sufficiently homogeneous for the chosen plan: same order, product identity, approved construction and relevant production conditions.
Do not quietly combine different colors, sizes, materials, artwork versions or production sources into one lot merely to reduce the sample size. If variants have different risks, the buyer may require separate lots or stratified sampling. The report should state exactly what was available and how variants were represented.
| Lot question | What the inspector should record |
|---|---|
| What goods are covered? | PO, SKU, style, color, size and artwork revision |
| How many units exist? | Presented quantity and packed quantity at inspection time |
| How are they packed? | Carton count, units per carton and assortment |
| Are there sublots? | Production date, line, material/print batch or supplier source where relevant |
| What is excluded? | Unfinished, quarantined, replacement or not-yet-present goods |
| Can the lot change later? | Controls preventing uninspected goods from entering the shipment |
How Should Buyers Use AQL Sampling?
Acceptance sampling is a statistical decision tool, not a quality guarantee. Under attribute sampling, inspected units or defects are classified as conforming/nonconforming, and the plan supplies a sample size plus acceptance/rejection criteria.
ISO 2859-1:2026 is the current edition for lot-by-lot attribute inspection using acceptance quality limit (AQL) schemes for a continuing series of lots. ISO states that the 2026 edition replaces the 1999 edition and its amendments. For an isolated lot or short series where the switching rules of Part 1 are not applicable, ISO 2859-2:2020 provides plans indexed by limiting quality.
The American route ANSI/ASQ Z1.4 also provides attribute sampling procedures for continuing streams of lots. The purchase contract must identify which standard and edition governs; mixing a code letter from one table with acceptance numbers from another is not valid.
AQL does not mean “the allowed percentage of defective bags”
An AQL-indexed plan controls lot-acceptance decisions over a continuing process under its rules. It is not permission to knowingly include that percentage of defective goods, and it does not mean the inspected sample represents the exact lot defect rate. A passed sample can still contain a defect, and an uninspected unit can be nonconforming.
Specify the entire plan, not only an AQL number
| Required sampling field | Why it matters |
|---|---|
| Governing standard and edition | Tables and rules can change between editions |
| Lot size and lot definition | Drives plan selection and defines decision scope |
| Normal, tightened, reduced or isolated-lot route | Different schemes have different purposes and rules |
| Inspection level/severity | Influences sample size and discrimination |
| Single, double or other plan | Changes the inspection sequence and decision points |
| Defect classes | Determines which defects are counted together |
| AQL or LQ for each class | Connects risk choice to acceptance/rejection numbers |
| Sample-selection method | Prevents convenient or biased samples |
| Disposition authority | Defines who may accept, reject or grant a concession |
This article intentionally does not reproduce proprietary sampling tables or prescribe default AQL values. Buyers should select the plan with a qualified quality professional and use an authorized copy of the chosen standard.
Select Cartons and Bags Randomly
Random selection is central to a credible final inspection. The inspector—not the packing team—should choose the cartons and units.
- Obtain the presented carton list and verify the physical count.
- Select cartons across different pallet positions, rows, production dates or packing zones where relevant.
- Avoid drawing the full sample from cartons already open for the inspector.
- Open selected cartons and choose units from different layers and positions.
- Preserve variant representation according to the written sampling instruction.
- Mark sampled cartons and record how goods were returned, repacked or quarantined.
Convenience sampling from the top of one carton can miss packing errors, late-production drift, mixed colors and defects hidden deeper in the lot.
Step 1: Verify Quantity, Assortment and Packaging
Start with the shipment configuration before inspecting individual bags.
| Checkpoint | What to compare | Possible nonconformity |
|---|---|---|
| Presented quantity | PO, packing list and physical cartons | Shortage, overage or unpresented balance |
| Units per carton | Approved pack-out | Incorrect count or inconsistent carton quantity |
| Variant assortment | Color/size/SKU packing plan | Mixed or missing variant |
| Unit packaging | Polybag, paper wrap, insert, warning or venting instruction | Wrong material, missing item or poor closure |
| Labels/barcodes | Approved artwork and scan/verification instruction | Wrong code, unreadable print or misplaced label |
| Export carton | Dimensions, board/construction and closure specification | Crushed, wet, open or unsuitable carton |
| Shipping marks | Approved mark and destination information | Incorrect destination, PO, carton number or handling mark |
Do not publish customer labels or shipping marks in a public report. Inspection evidence may contain confidential PO, consignee and product information and should remain within the authorized order file.
Step 2: Inspect Appearance and Workmanship
Inspect bags under consistent lighting and from the agreed viewing distance. Separate genuine defects from natural material characteristics defined in the approved reference.
Fabric and cleanliness
Check holes, cuts, snags, stains, oil, dust, foreign matter, excessive creasing, discoloration and unacceptable odor. For natural cotton or jute-like materials, allowable slubs, shade variation or fiber characteristics should be defined rather than judged retrospectively.
Sewing and edge finishing
Look for open seams, skipped stitches, broken thread, loose or unsecured ends, seam puckering, needle damage, raw edges, incorrect seam allowance and inconsistent stitch path. Inspect high-stress cord-channel and lower-corner areas carefully.
Symmetry and shape
Lay the bag flat without stretching. Compare body shape, top line, side/bottom gusset alignment, corner symmetry and panel matching with the approved sample.
Hardware and accessories
Where present, examine eyelets, cord locks, zippers, pockets, labels, snaps, lining and reinforcement patches. Confirm correct type, color, orientation, security and surface condition.
Step 3: Measure Dimensions Correctly
Measurement disputes often come from an undefined method rather than a real production error.
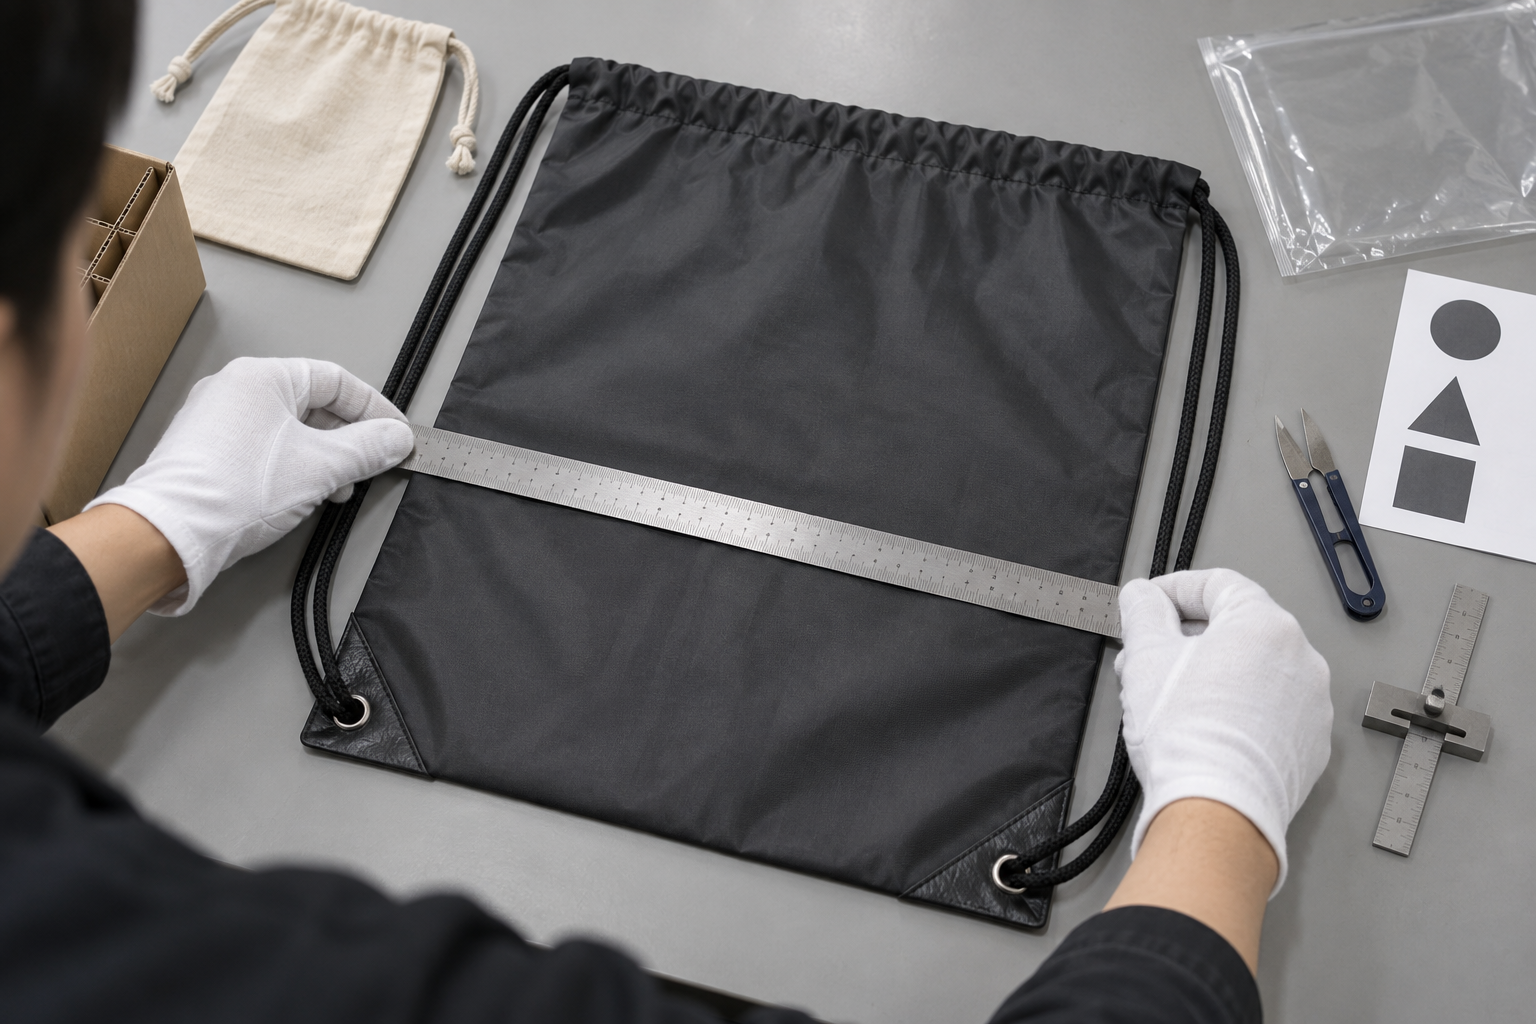
Editorial visualization of dimension and construction checks on a generic bag. It does not show an actual LUCKYSTAR inspection, calibrated-equipment record or approved customer specification.
Before measuring, define whether the bag is conditioned, flattened, tension-free, opened, filled or otherwise prepared. Use the same width × height × gusset order and reference points as the specification.
| Measurement | Method detail to freeze |
|---|---|
| Body width | Between specified side edges, flat and without stretching |
| Body height | From the defined top/bottom points; state whether cord channel is included |
| Side or bottom gusset | Folded or fully opened method and measuring points |
| Cord length | Free length, loop length or end-to-end route |
| Print dimensions | Artwork boundary, visible image or transfer-film boundary |
| Print placement | Distance from defined bag edges, seam, fold or centerline |
| Pocket/zipper/label position | Reference edge and orientation |
Record individual results, not only an average. An average within tolerance can hide out-of-tolerance units. The Drawstring Bag Size and Capacity Guide provides additional specification context.
Step 4: Confirm Material, Color and Branding
Final inspection can compare observable characteristics with approved references, but visual inspection alone cannot prove fiber composition, recycled content, coating chemistry or regulatory compliance.
| Attribute | Final inspection can check | Separate evidence that may be needed |
|---|---|---|
| Fabric type/handfeel | Apparent match to approved sample | Material certificate, composition test or supplier record |
| Weight/thickness | Agreed measurement on sampled material where practical | Calibrated method and lot-specific data |
| Color | Visual or instrument comparison under defined conditions | Color tolerance and controlled illuminant/method |
| Print/embroidery | Artwork, size, location, color and visible defects | Adhesion, abrasion, crocking or wash testing |
| Recycled/organic claim | Correct approved label and document reference | Valid scope/transaction documentation for the order |
| Chemical compliance | Correct report identity and sample/lot linkage | Current qualified laboratory report and applicable legal assessment |
Never convert the existence of an old report into a pass for a current shipment. Certificates and reports must match the legal entity, product/material, test scope, date and order requirements.
Step 5: Check Drawcords, Eyelets and Reinforcements
The closure system is a defining feature of a drawstring bag.
Functional checks
- pull both sides through the full closing and opening travel;
- confirm the channel does not bind, twist or trap the cord;
- verify cord length and left/right symmetry;
- inspect knots, aglets or heat-sealed ends as specified;
- confirm cord locks operate and orient correctly where used;
- check that the opening reaches the specified usable width.
Construction checks
- eyelets are present, matched, seated and free from unacceptable sharp edges;
- fabric-reinforced corners are correctly shaped and fully stitched;
- cord attachment or routing matches the approved sample;
- pulling does not expose open seams or immediate tearing;
- metal finish and color match the approved specification where applicable.
For deeper engineering detail, see Drawstring Cord, Eyelet and Reinforcement Guide and Drawstring Cord Strength and Pull Test Guide.
Step 6: Perform the Agreed Functional Tests
The test list should be decided before production. Final inspection is not the right moment to invent a severe test that the sample and specification never addressed.
| Test | Purpose | Variables that must be written |
|---|---|---|
| Drawstring operation | Confirm smooth and complete closure/opening | Repetitions, fill state and failure definition |
| Static or dynamic load | Evaluate complete-bag construction under intended load | Mass, contents, duration/cycles, suspension and acceptance |
| Cord pull/attachment | Evaluate cord, knot, channel, eyelet or corner system | Loading route, force/rate, endpoint and damage limit |
| Seam check | Examine seam integrity at defined locations | Method, direction, load and acceptance |
| Print adhesion/rub | Evaluate decoration bonding or transfer | Method, contact, force/cycles and rating |
| Colorfastness | Evaluate staining or color change | Standard, dry/wet route and grade |
| Wash/dry | Support an agreed care claim | Complete wash/dry procedure, cycles and criteria |
| Zipper/pocket/accessory | Confirm operation and attachment | Repetitions, load and defect definition |
Destructive tests consume or damage samples. State how many units are tested, whether they are replaced, and whether failures count in the attribute sample or under a separate technical requirement.
Related detailed guides include How to Test Drawstring Bag Load Capacity, Drawstring Bag Print Adhesion and Abrasion Testing, Polyester Drawstring Bag Colorfastness Testing and Cotton Drawstring Bag Shrinkage and Washing Tests.
Adapt the Checklist to the Bag Material
| Material/construction | Additional final-inspection attention |
|---|---|
| Polyester or nylon | Snags, heat damage, coating variation, seam puckering and dye/print migration symptoms |
| Cotton or canvas | Slubs/characteristics versus defects, loose fibers, shade, shrinkage evidence where required |
| Non-woven PP | Heat-bond/seam consistency, tearing at stress points, surface disturbance and print adhesion |
| Mesh | Hole/mesh consistency, snagging, bound edges and stress concentration at cord attachment |
| Velvet or microfiber pouch | Pile direction, pressure marks, lint, embroidery backing and surface contamination |
| Coated/water-resistant fabric | Coating damage, seam route, delamination, blocking and claim-specific test evidence |
A material name alone does not establish a performance level. The inspection criteria must follow the selected material, construction, decoration and use.
Classify Defects Before the Inspection
Critical, major and minor are decision categories, not adjectives for how unpleasant a defect looks. The buyer should define them by product risk and intended use.
| Defect class | General decision logic | Drawstring bag examples that may fall in the class* |
|---|---|---|
| Critical | Could create an unacceptable safety, legal or prohibited-condition risk | Sharp exposed component, prohibited foreign object, wrong safety warning where legally required |
| Major | Likely to cause functional failure, sale rejection or material departure from specification | Open structural seam, missing cord, wrong SKU/artwork, unusable closure, materially out-of-tolerance size |
| Minor | Does not usually prevent use but departs from appearance/workmanship criteria | Small removable thread, limited cosmetic mark or slight nonfunctional asymmetry within defined limits |
*The table is illustrative only. The buyer's approved defect list governs classification. A defect can move between classes depending on the market, product use, artwork, packaging and contract.
Avoid double counting without a written rule. One bag with an open seam and a print defect may be one nonconforming unit with multiple nonconformities; the chosen sampling model must state how counting works.
Record Results So Another Person Can Reconstruct the Decision
A final report should contain more than a few attractive photos.
Lot and sampling record
- inspection date, location and responsible parties;
- order/SKU/variant and presented quantities;
- production and packing completion status;
- lot/sublot definition and carton distribution;
- governing sampling plan and exact parameters;
- cartons and units selected.
Product findings
- checklist results and individual measurements;
- defect count by class and clear defect descriptions;
- functional/destructive test conditions and outcomes;
- comparison with approved samples and specifications;
- photographs showing both overview and close-up context.
Shipment and disposition record
- unit pack, assortment, carton and shipping-mark results;
- missing documents or unresolved questions;
- accept/reject/hold recommendation;
- authorized final decision and any concession;
- corrective action, rework quantity and reinspection plan.
Sensitive customer logos, barcodes, addresses, order data and reports should not be reused as public marketing material without explicit authorization.
What Happens After a Failed Inspection?
A failed sample should trigger containment and root-cause work—not cosmetic editing of the report.
- Hold the defined lot. Prevent loading or mixing with other goods.
- Confirm the finding. Check method, reference and equipment without erasing valid defects.
- Map the scope. Identify affected SKUs, colors, cartons, shifts, lots or processes.
- Choose a disposition. Rework, sort, replace, remake, accept by written concession, or reject.
- Correct the cause. Address printing, sewing, material, packing, training or document control as applicable.
- Verify the correction. The original failed sample does not become a pass because selected defects were removed.
- Reinspect under the agreed rule. Define whether a new lot is formed and which sampling plan applies.
- Update shipment documents. Quantity, carton count and packing list must reflect the corrected lot.
Conditional acceptance belongs to the buyer's authorized process. The supplier or inspector should not silently downgrade a defect or change an AQL to achieve a pass.
Pass, Hold, Conditional Acceptance and Reject
| Disposition | Appropriate meaning | Required evidence |
|---|---|---|
| Pass | Sample results satisfy the agreed release criteria | Complete report and shipment identity control |
| Hold | Information, test result or correction remains pending | Hold notice, responsible party and closure condition |
| Conditional acceptance | Buyer knowingly accepts a documented deviation | Written concession identifying scope and commercial impact |
| Rework/reinspect | Lot requires correction and a new verification decision | Rework record, lot control and reinspection plan |
| Reject/remake | Lot does not meet requirements and is not accepted | Defect evidence, disposition and revised delivery plan |
An inspector's “pass” is limited to the inspected lot, sample and criteria. It is not a certification of all future orders or a guarantee that every uninspected unit is conforming.
Why Choose LUCKYSTAR for Custom Drawstring Bag Programs?
LUCKYSTAR supports custom bag projects from requirement collection and sample development through production coordination, inspection and shipment preparation. The practical value is a traceable handoff between the buyer's specification, approved sample and final release record—not an unsupported claim that one generic checklist fits every order.
| LUCKYSTAR project support | Procurement value |
|---|---|
| Collect material, dimensions, artwork, cord, reinforcement, packing and target-market requirements | Reduces ambiguity before quotation and sampling |
| Coordinate a production-intent sample and written revisions | Creates a controlled comparison reference |
| Translate buyer requirements into incoming, first-article, in-process and final checkpoints | Places controls where defects can be detected earlier |
| Define order-specific testing and reporting needs | Separates visual inspection from technical or laboratory evidence |
| Review packing, carton and shipment-document requirements | Reduces last-stage logistics errors |
| Retain project evidence subject to agreed scope and authorization | Supports complaints, reorders and corrective action |
Materials, minimum order quantity, sampling plan, inspection scope, testing, lead time, documentation and commercial terms remain subject to the final specification and written confirmation. For supplier qualification, read the drawstring bag manufacturer selection guide and the broader Custom Bag Manufacturer Guide.
Buyer’s Pre-Shipment Inspection Brief
Send this information before inspection is booked:
| Brief field | Buyer input |
|---|---|
| Order identity | PO, SKU, color/size variants and destination |
| Lot | Quantity, sublot rules, production status and packing threshold |
| References | Final specification, approved sample, artwork and packing files |
| Sampling | Standard/edition, scheme, inspection level and defect-class criteria |
| Checks | Workmanship, measurement, color, print, cord, reinforcement and accessories |
| Tests | Method, sample quantity, equipment, conditions and acceptance limit |
| Packaging | Unit pack, assortment, barcode, carton and shipping marks |
| Evidence | Required photographs, measurements, test records and report format |
| Disposition | Authorized approver, hold rule, concession route and reinspection rule |
The Custom Drawstring Bag Manufacturing Process shows where this release gate fits within the complete order workflow, while the sample development guide explains how the comparison reference is established.
Frequently Asked Questions
When should a pre-shipment inspection take place?
It should occur when the defined lot is complete enough to represent the actual shipment and final packing is available according to the written inspection instruction. The exact completion threshold is an order-level decision, not a universal percentage.
Does passing an AQL inspection mean every bag is defect-free?
No. Acceptance sampling supports a lot decision from a sample. It does not inspect every unit and does not guarantee zero defects in the uninspected population.
Which AQL should be used for drawstring bags?
There is no universal drawstring-bag AQL. The buyer should choose the sampling standard, edition, inspection scheme and class-specific limits according to product risk, process history and commercial requirements.
Can different colors be combined into one sample?
Only if the lot definition and sampling instruction allow it and the sample represents each variant appropriately. Different materials, artwork, print systems or production conditions may justify separate sublots or samples.
Should dimensions be averaged?
Keep individual measurements. An acceptable average can hide units outside tolerance. The specification should define preparation, measurement points and the decision rule.
Are load and cord-pull tests part of every final inspection?
Only when they are specified. Define load, duration/cycles, fixture, sample quantity, endpoint and whether the test is destructive. A vague “strength test” is not repeatable.
Can an inspector verify recycled content or fiber composition visually?
No. Visual comparison can identify an obvious mismatch, but composition and recycled-content claims require appropriate traceable documentation and, where required, testing or certification tied to the order.
What should happen if goods fail inspection?
Hold the lot, identify the affected scope, correct or disposition the goods through authorized channels, and reinspect under the agreed rule. Do not ship first and resolve the report later.
Is an inspection report the same as a product certificate?
No. An inspection report records observations and results for the identified lot and scope. A certificate or laboratory report has its own issuer, method, subject, validity and coverage requirements.
Can LUCKYSTAR arrange final inspection requirements?
LUCKYSTAR can coordinate order-specific inspection requirements, sampling instructions, reference documents and reporting options. The exact scope, inspector, tests, timing and commercial responsibility must be confirmed in writing for the individual project.
Final Pre-Shipment Decision
A defensible release decision connects five things: a frozen specification, a clearly identified lot, an appropriate sampling plan, reproducible checks and an authorized disposition. Missing any one of them weakens the conclusion.
Send LUCKYSTAR your bag specification, artwork, quantity, variant plan, packing requirements, destination and inspection criteria early in the project. That allows the approved sample, production checkpoints and final report to use the same definitions.
Request a custom drawstring bag quotation and attach your inspection brief or current quality manual. All product specifications, sampling plans, tests, commercial terms and shipment commitments are subject to review and written confirmation.
Technical References
- International Organization for Standardization. ISO 2859-1:2026 — Sampling procedures for inspection by attributes, Part 1: AQL-indexed schemes for lot-by-lot inspection. Current edition checked September 28, 2026.
- International Organization for Standardization. ISO 2859-2:2020 — Sampling plans indexed by limiting quality for isolated lot inspection. Status checked September 28, 2026.
- American Society for Quality. ANSI/ASQ Z1.4 and Z1.9 overview. Edition information checked September 28, 2026.