Drawstring Bag Print Adhesion and Abrasion Testing
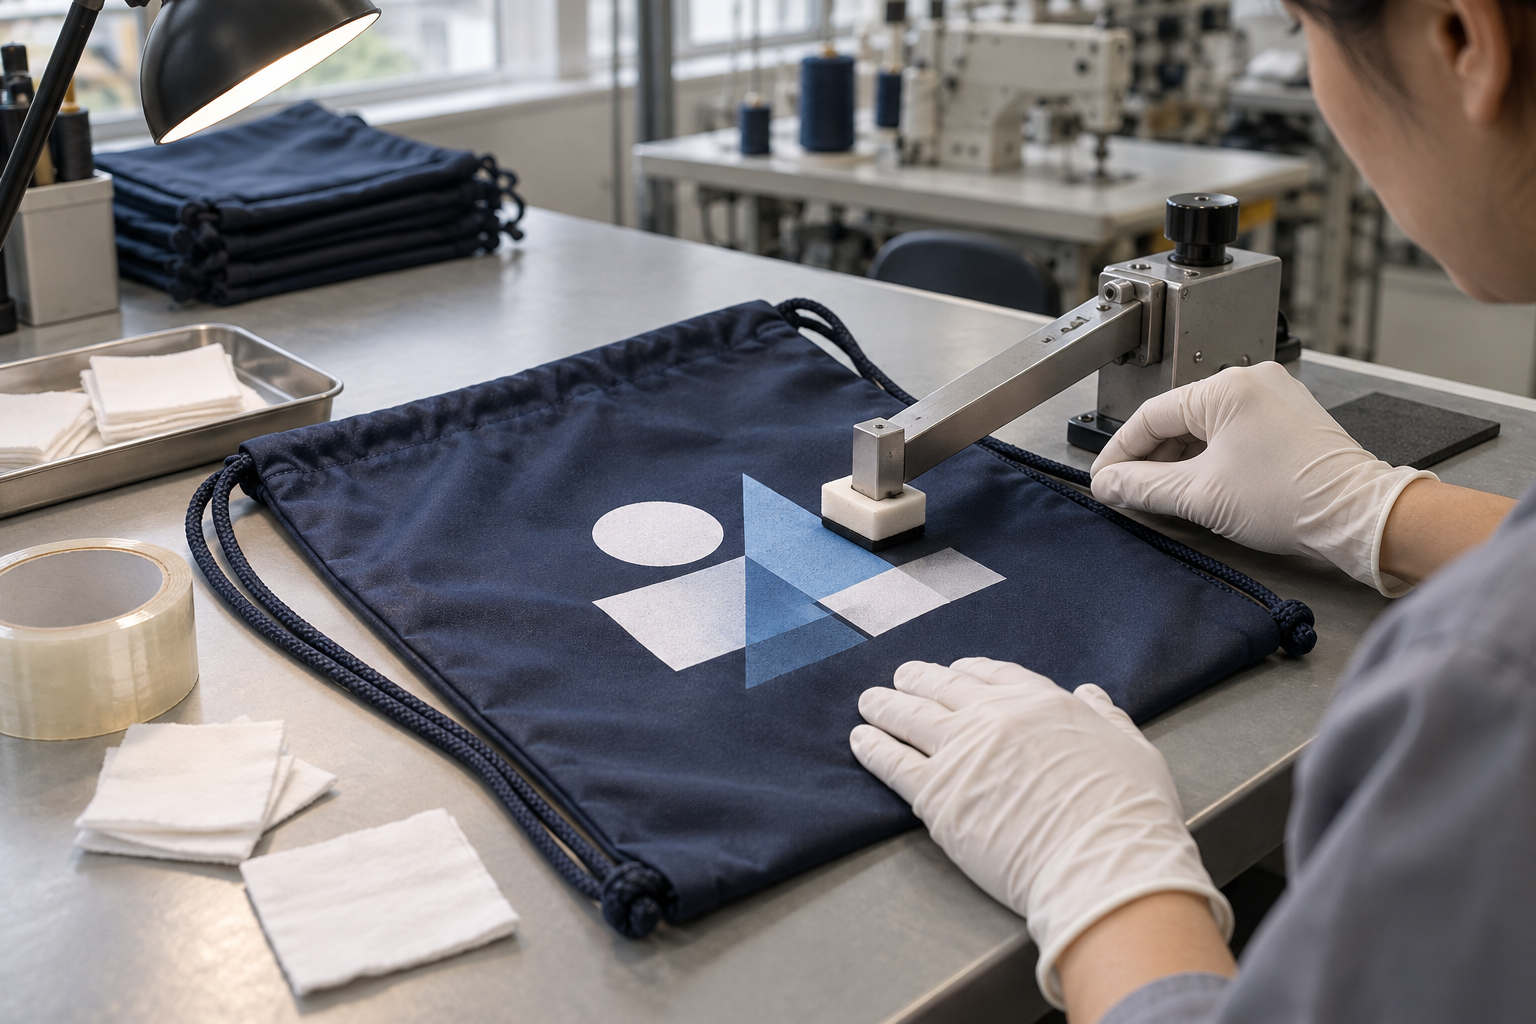
Editorial visualization of a controlled rubbing check on an unbranded drawstring bag. It illustrates a test workflow and is not a documented customer order, proprietary laboratory method, or LUCKYSTAR test result.
The short answer: drawstring bag print quality should not be approved with one generic “rub test.” A useful validation plan separates adhesion (whether ink or film remains bonded to the bag), crocking or color transfer (whether color rubs onto another material), and abrasion resistance (how the printed surface changes after repeated contact). The buyer and manufacturer must also define the bag material, print system, conditioning, contact material, force, cycle count, wet or dry state, evaluation method, and acceptance limit before testing.
This distinction matters because a print can pass one check and fail another. A heat-transfer film may show little color transfer yet lift at an edge. A screen print may remain attached but become polished, cracked, or visibly worn. A dark ink may look intact while staining a white rubbing cloth. None of these outcomes can be summarized reliably as simply “the logo passed.”
For custom programs, the practical objective is to convert the intended use into a repeatable, order-specific test plan. Buyers reviewing custom drawstring bags can use the framework below to write that plan before sample approval and mass production.
What Do Print Adhesion and Abrasion Tests Actually Measure?
The three terms are related, but they answer different questions.
| Quality question | Property being examined | Typical evidence | What the result does not prove |
|---|---|---|---|
| Does the printed layer stay attached? | Adhesion between print system and substrate | Edge lifting, film removal, flaking, exposed fabric | Resistance to long-term rubbing or washing |
| Does color transfer during rubbing? | Dry or wet crocking/colorfastness to rubbing | Staining on a specified rubbing cloth and change on the specimen | Mechanical adhesion of a transfer film |
| Does the graphic remain acceptable after contact? | Abrasion/scuff resistance | Gloss change, wear-through, loss of detail, cracking, haze | Performance in every real-use environment |
| Does bending damage the decoration? | Flex resistance of the print-and-fabric system | Cracks, whitening, edge separation after folding or crumpling | Resistance to planar abrasion under a machine |
| Does cleaning affect the decoration? | Wash or wipe durability | Post-cleaning cracking, fading, transfer or peeling | Suitability for an unspecified care process |
The unit under test is not only the ink. It is the full system: substrate fiber, weave or coating; pretreatment; ink, adhesive or transfer film; curing conditions; print thickness; artwork coverage; and post-print handling. Changing one layer can change the outcome.
Is There One Standard for Drawstring Bag Print Adhesion?
No single international standard supplies a universal pass/fail requirement for every printed drawstring bag. Standards normally define a method or apparatus for a particular material and property. The purchase specification still has to select the method and set an acceptance limit appropriate to the product.
| Reference | What it addresses | Appropriate use in a bag program | Important boundary |
|---|---|---|---|
| ISO 105-X12:2016 | Colorfastness of textiles to dry and wet rubbing | Evaluate color transfer from dyed or printed textile surfaces | It is a rubbing colorfastness method, not a film-adhesion test |
| AATCC TM8 | Colorfastness to crocking using a Crockmeter | Alternative buyer-specified route for dry/wet crocking | Method designation alone does not create a universal bag grade |
| ASTM D3359-23 | Tape rating of relatively ductile coatings, developed for metallic substrates | A conceptual reference when building a controlled internal tape screen | ASTM states the method was developed with metal as the substrate; it must not be represented automatically as a textile-bag test |
| ISO 5470-1:2016 | Taber abrasion of rubber- or plastics-coated fabrics | Potentially relevant to suitable coated bag materials | It addresses coated-fabric abrasion, not every ink on every textile |
| ASTM D4966-22(2026) | Martindale abrasion resistance of textile fabrics | Comparative development work when the specimen and holder are suitable | ASTM notes abrasion results can vary and does not recommend the method as a simple commercial-shipment acceptance test |
| ASTM D5264-98(2019) | Sutherland rub resistance of printed materials | May inform testing of flat, packaging-like printed panels | Its stated scope centers on labels, cartons and other flat packaging substrates, so applicability to a flexible finished bag must be agreed |
The correct wording is therefore “tested according to the agreed method and acceptance criteria,” not “abrasion-proof,” “permanent print,” or “certified by ISO.” ISO publishes standards; it does not certify an individual bag through use of a test-method number.
Start With the Bag’s Real Print System
The same logo can behave differently on cotton, polyester, nylon, non-woven polypropylene, mesh, or a coated fabric. The method should follow the actual construction, rather than forcing every bag into one laboratory routine.
| Bag and decoration combination | Main risks to investigate | Useful development checks |
|---|---|---|
| Screen ink on cotton or canvas | Fiber movement, uneven ink holdout, cracking over coarse yarns | Adhesion screen, flexing, dry/wet rubbing, wash test if claimed washable |
| Screen ink on polyester | Surface finish incompatibility, incomplete cure, dye migration | Cure verification, adhesion, crocking, heat-aging comparison where relevant |
| Heat-transfer film on polyester | Edge lift, adhesive failure, cracking, heat marks | Edge inspection, tape screen, flex/crumple, repeated rubbing, wash route if applicable |
| Sublimation on suitable polyester | Image color change or transfer rather than film lift | Crocking, washing where relevant, color comparison, migration risk review |
| Printed non-woven PP | Low surface energy, fiber disturbance, coating/ink mismatch | Pretreatment confirmation, adhesion screen, bend and rub checks |
| Reflective transfer | Segment lift, cracking, change in reflective appearance | Adhesion, flex, abrasion and performance testing specified by intended use |
| Full-surface printed panel | Wear at seams, folds, cord channel and bottom contact areas | Panel test plus complete-bag handling simulation |
For a broader process comparison, see Custom Drawstring Bag Printing Methods, Screen Printing vs Heat Transfer for Drawstring Bags, and Sublimation vs Screen Printing for Polyester Drawstring Bags.
Define the Failure Mode Before Selecting the Test
“Print failure” is too broad for a corrective action. A useful report identifies where and how failure occurred.
Adhesive failure
The printed layer separates from the bag surface. A transferred film may lift cleanly from the textile, or an ink layer may flake away and reveal the substrate. Potential causes include incompatible chemistry, insufficient surface preparation, contamination, unsuitable temperature/pressure/time, or incomplete cure.
Cohesive failure
The decoration splits within itself while some material remains bonded to the bag. This may appear as cracking, powdering, tearing, or separation between layers of a multilayer transfer. The interface may be sound even though the film or ink body is not durable enough for the intended flexing.
Substrate failure
Fibers pull away with the print or the base material tears before the decoration releases. This is not automatically a “good adhesion” result; it means the weakest point moved into the substrate. Buyers should record the actual failure location rather than assigning a generic pass.
Color transfer without visible delamination
Pigment or dye stains the rubbing cloth even when the graphic still appears attached. Dry and wet transfer can differ substantially. The result belongs under colorfastness/crocking, not mechanical peel adhesion.
Surface wear without detachment
Abrasion may reduce gloss, blur fine artwork, expose high points in the textile weave, or create haze before any layer peels. A buyer concerned with brand appearance may reject this change even when the print remains bonded.
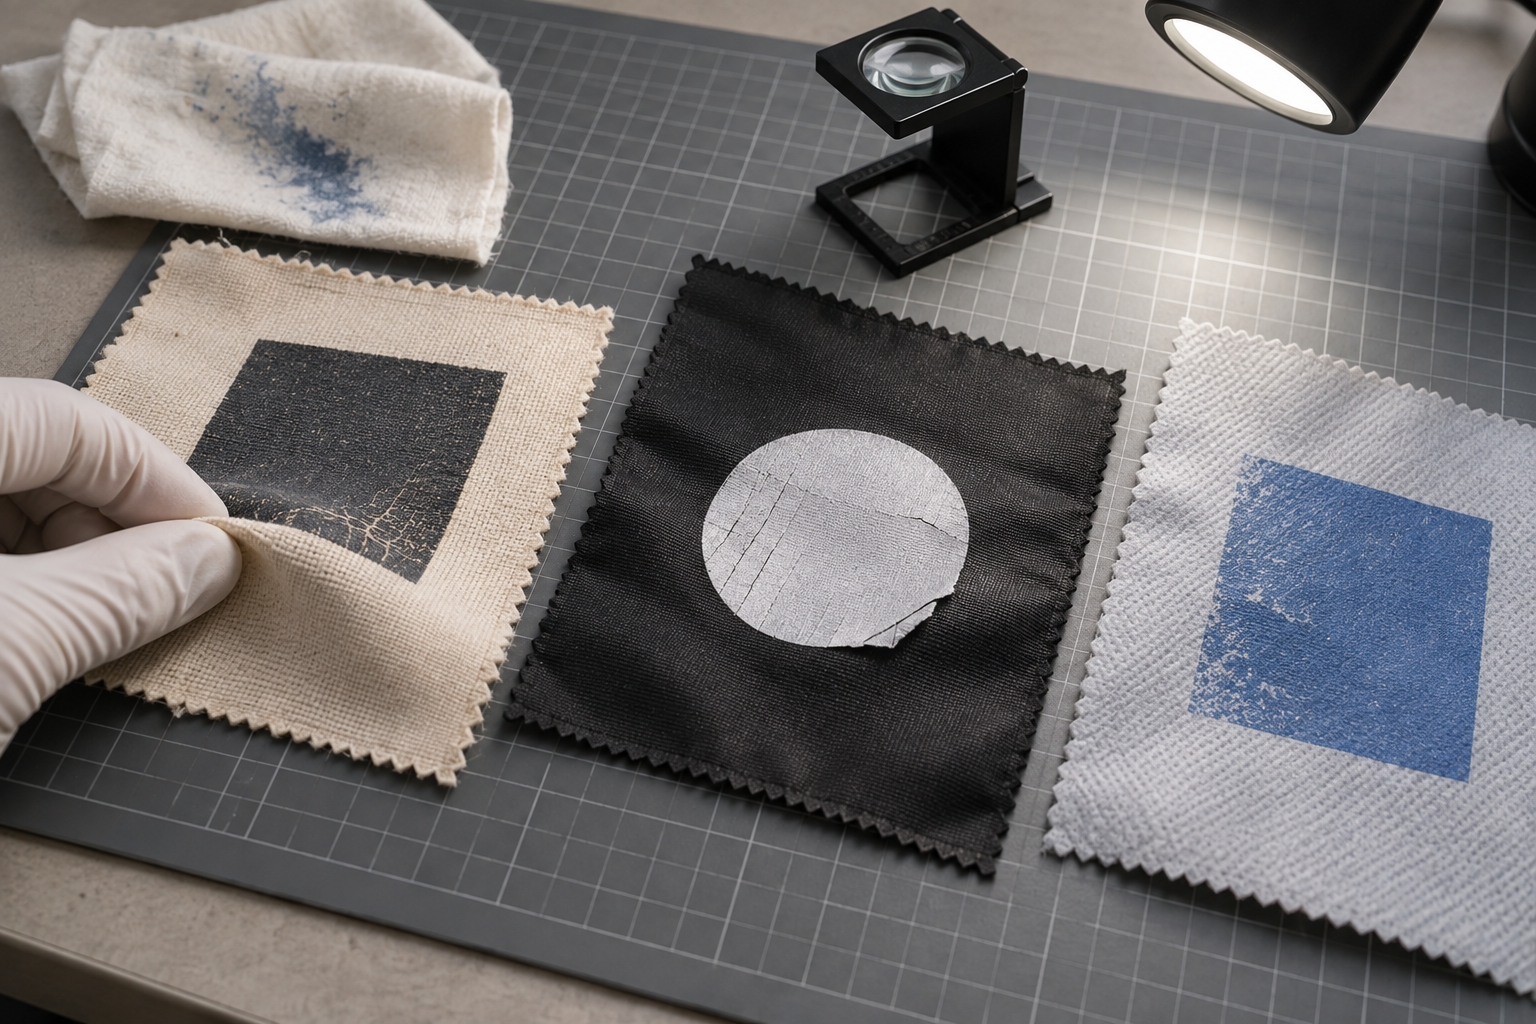
Editorial visualization of restrained defect patterns on generic textile swatches. The image is not a laboratory result, approved sample, or evidence of a particular production batch.
Build a Repeatable Test Specimen Plan
Testing random offcuts is not enough if the production bag contains seams, drawcord channels, folds, coatings or multiple colors. Use both flat development panels and completed bags where practical.
| Specimen decision | What to specify | Why it matters |
|---|---|---|
| Production intent | Final substrate, color, finish, pretreatment, ink/film and curing route | A white lab swatch may not represent a dyed production fabric |
| Artwork | Solid blocks, fine lines, reversed text, halftones and large coverage where used | Different graphic elements reveal different failure mechanisms |
| Print location | Center panel, near seam, near bottom, over fold or close to cord channel | Geometry changes pressure, flexing and wear |
| Quantity | Replicates from more than one print position or run point | One specimen cannot show variation |
| Conditioning | Time, temperature and humidity before testing | Freshly printed material may continue curing or equilibrating |
| Control | Approved reference sample or untested duplicate | Provides a visual baseline for change |
| Identification | Sample code, date, ink/film batch, operator and cure record | Enables root-cause analysis and reorder control |
The approved sample should be connected to the artwork and process specification. The drawstring bag artwork and dieline guide explains why safe areas, seams and full-surface coverage must be resolved before the test piece is produced.
A Practical Print Adhesion Test Workflow
The following workflow is a specification template, not a universal standard.
1. Condition and identify the samples
Allow the print to reach the agreed post-production condition. Record the interval after printing, because testing immediately after cure and testing after storage may produce different results. Photograph the untested surface under consistent light.
2. Inspect at normal and raking light
Check pinholes, incomplete coverage, edge lift, bubbles, contamination, blocking, excessive gloss variation and print-through. Raking light helps reveal raised edges and fine cracks that are difficult to see head-on.
3. Apply the agreed tape screen only when appropriate
If a buyer and supplier use an internal tape-pull screen, define the tape, storage condition, contact time, application pressure, pull angle, pull rate, whether the print is cut, and the rating rule. Flexible or porous textiles can distort, release fibers, or respond differently to different tape adhesives.
A casual office-tape pull is useful only as an informal warning check. It is not reproducible evidence unless all variables are controlled. ASTM D3359 should not be claimed as direct proof for a textile bag unless the parties have confirmed applicability and followed the actual standard within its scope.
4. Bend and flex the decorated area
Fold or flex the printed panel in the directions that occur during packing and use. Examine for whitening, cracking, edge separation and loss at high textile points. Record the fold geometry and number of repetitions if the result is used for acceptance.
5. Test representative weak points
Large solid areas, sharp corners, narrow lines and edges near seams can fail differently. Do not perform the adhesion screen only in the easiest center area and then approve the full graphic.
6. Classify the failure
Record adhesive, cohesive, substrate or mixed failure. Include close photographs and the exact tested location. “Peel observed” without a failure description gives the printer little information for correction.
A Practical Dry and Wet Rubbing Workflow
ISO 105-X12 and AATCC TM8 provide recognized routes for evaluating textile color transfer by rubbing. The exact standard, edition, apparatus, test direction, wet pickup or preparation details, rubbing cloth and evaluation scale must come from the controlled test specification or laboratory instruction.
- Select the agreed test method and current edition.
- Condition the printed specimen and rubbing material as required.
- Test the defined print areas and directions.
- Run dry and wet routes when both are relevant to expected use.
- Evaluate staining of the rubbing cloth and change to the specimen using the agreed assessment procedure.
- Record whether the observed issue is transferred color, surface wear, or both.
Wet rubbing is not simply dry rubbing with an arbitrarily damp cloth. Moisture content and preparation affect friction and color transfer. A buyer should not compare results from two suppliers unless the procedures are genuinely equivalent.
How to Design an Abrasion or Scuff Test
Abrasion results are highly method-dependent. A cycle count without the rest of the conditions is incomplete.
| Variable | What the specification should state | Typical consequence if omitted |
|---|---|---|
| Apparatus or motion | Linear rub, rotary rub, Martindale, Taber, bag-to-bag scuff or other agreed route | Results cannot be compared |
| Abradant/contact surface | Standard textile, rubber, paper, fabric, finished bag surface or other material | Wear mechanism changes |
| Force/load | Applied mass, pressure or machine setting | More force can accelerate damage |
| Stroke or path | Length, direction and contact area | A seam or weave direction may be missed |
| Cycles | Inspection intervals and final endpoint | “Passed abrasion” has no defined exposure |
| Specimen mounting | Tension, backing and flatness | Wrinkling can concentrate contact |
| Environment | Conditioned, wet, heated, cooled or chemically exposed | Print and adhesive behavior may change |
| Evaluation | Visual grade, color difference, mass loss, image loss or defined defect limit | Operators may reach different conclusions |
| Replicates | Quantity and sampling locations | One result may hide variation |
For an everyday promotional bag, a controlled bag-to-bag scuff simulation may represent packing and transport better than a high-cycle material test. For coated fabric, ISO 5470-1 or another coated-fabric method may be relevant. For textile panels, a Martindale-based comparison may help development, but ASTM D4966 explicitly warns about variability and commercial-shipment acceptance. The selection must follow the material and failure risk.
Add Real-Use Simulation at Finished-Bag Level
Laboratory panels isolate a property; completed bags reveal interactions.
| Simulation | What it can reveal | Required control |
|---|---|---|
| Repeated opening and closing | Cord-channel rubbing across a nearby print | Fill state, repetitions and cord route |
| Fold-and-pack cycle | Cracking or transfer where bags are compressed | Fold pattern, dwell time and stack pressure |
| Bag-to-bag transit scuff | Surface polishing, transfer and wear at raised points | Orientation, load, vibration or movement |
| Filled carry cycle | Distortion and print cracking under body stretch | Fill mass, contents, duration and bag dimensions |
| Wipe-clean simulation | Sensitivity to cleaner or wet cloth | Liquid, concentration, cloth and strokes |
| Wash-and-dry route | Durability when a washable claim is intended | Complete wash/dry procedure and number of cycles |
If the bag is marketed as washable, connect print evaluation to a defined wash procedure. ISO 6330:2021 specifies multiple domestic washing and drying procedures; it does not mean every procedure is suitable for every drawstring bag. The care instruction, substrate, decoration and intended market must agree.
How Should Buyers Set Acceptance Criteria?
Acceptance criteria should reflect a visible, functional or regulatory requirement. They should be agreed before testing—not invented after the sample fails.
| Test item | Buyer-defined method field | Buyer-defined acceptance field |
|---|---|---|
| Initial appearance | Lighting, viewing distance, reference sample | No listed critical defect; defined tolerance for minor defects |
| Adhesion screen | Tape/procedure or other method, locations, conditioning | Maximum permitted lift/removal and failure classification |
| Dry crocking | Standard and method details | Minimum agreed staining/change grade |
| Wet crocking | Standard and method details | Minimum agreed staining/change grade |
| Flex test | Fold radius/direction, repetitions, inspection | Maximum crack, whitening or edge-lift limit |
| Abrasion/scuff | Apparatus, abradant, load, cycles, mounting | Maximum image loss, color/gloss change or wear area |
| Cleaning/washing | Complete cleaning or wash/dry route, cycle count | Maximum cracking, peeling, fading, transfer and dimensional effect |
| Finished-bag simulation | Fill, folding, packing, rubbing and duration | No critical loss of branding or defined cosmetic limit |
Numeric limits should come from the buyer's use case, approved sample, applicable standard, market requirement, or qualified laboratory plan. LUCKYSTAR should not substitute a generic internet value for the customer's performance requirement.
Sampling: Development, First Article and Production
Print validation should occur at more than one stage.
Development sample
Compare ink, transfer, pretreatment and cure alternatives. Use worst-case fabric colors and high-coverage artwork where they create additional risk. The goal is to choose a viable process, not to prove mass-production consistency.
Pre-production or golden sample
Freeze the substrate, decoration, artwork, location, color target and evaluation criteria. The approved sample should be signed or otherwise traceably approved. See Custom Drawstring Bag Sample Development Process.
First production article
Confirm that production settings reproduce the approved result before the full run proceeds. Record cure conditions and the actual material/ink or film lots where traceability is required.
In-process and final inspection
Monitor appearance, placement and obvious adhesion symptoms during production. Perform destructive tests only according to the agreed sampling plan because tested units may no longer be saleable. The Custom Drawstring Bag Quality Control Checklist provides the wider inspection context.
Common Failure Patterns and Corrective Questions
| Observed result | Possible contributors to investigate | Corrective questions |
|---|---|---|
| Film lifts at corners | Insufficient pressure, low surface energy, sharp artwork corner, contamination | Was pretreatment controlled? Were time, temperature and pressure recorded? |
| Ink rubs off soon after printing | Incomplete cure, incompatible ink, excess deposit, early handling | Was cure verified across the full dryer/press area? Was the sample aged before testing? |
| Print cracks when bag is folded | Brittle print layer, excessive thickness, unsuitable film, coarse substrate | Can artwork coverage or print system change without losing brand intent? |
| Wet rubbing stains heavily | Pigment/dye migration, binder limitation, insufficient cure | Is wet use expected? Is the chosen color/fabric/ink combination suitable? |
| Only seam-side graphic wears | Uneven contact, raised seam, poor artwork placement | Should the print move farther from construction features? |
| Fine details disappear before solid areas | Thin deposit, artwork resolution, uneven substrate contact | Were the smallest production features included in the approved sample? |
| Transfer remains intact but fabric tears | Strong bond on weak or damaged substrate | Is the base material appropriate for the intended use and test severity? |
| Results vary between operators | Undefined pressure, speed, angle, moisture or visual criteria | Can the method be standardized and operators trained with reference samples? |
For artwork that approaches seams or covers most of the panel, also review How to Print Full-Surface Graphics on Drawstring Bags. Reflective graphics need additional application-specific evaluation described in Reflective Printing for Sports Drawstring Bags.
What Should Be in the Test Report?
A pass/fail label without traceability is weak evidence. A useful report should include:
- product and sample identification;
- bag material, color, coating or finish;
- print process, ink/film system and artwork version;
- production or sample date and relevant curing record;
- conditioning and pre-treatment information;
- standard/method name, edition and any deviations;
- apparatus, contact material, force/load, path and cycles;
- wet/dry or cleaning conditions;
- specimen location and number of replicates;
- before/after images under consistent lighting;
- numerical or visual results and acceptance criteria;
- failure type and tested-sample disposition;
- operator, date and laboratory or inspection location.
Third-party laboratory accreditation, when required, should be scoped to the relevant test. A laboratory logo by itself does not prove that a particular method or sample is covered.
Why Work With LUCKYSTAR on Printed Drawstring Bags?
LUCKYSTAR supports custom bag development from requirement collection through sampling, production coordination, inspection and shipment. For print-durability projects, the useful advantage is not an unsupported promise that every decoration is permanent. It is the ability to organize the specification so the buyer, sample team and production team evaluate the same construction.
| LUCKYSTAR project step | Buyer benefit |
|---|---|
| Collect substrate, artwork, use, care and target-market requirements | Prevents the print method from being selected by artwork appearance alone |
| Compare screen printing, heat transfer, sublimation and other feasible routes | Aligns process choice with material, coverage and expected handling |
| Develop and document a production-intent sample | Creates a physical reference before mass production |
| Define inspection points and order-specific tests | Separates appearance, adhesion, crocking and abrasion decisions |
| Coordinate first-article and in-process checks | Helps detect cure, placement or handling variation earlier |
| Retain approval and inspection evidence subject to project scope | Supports reorder communication and root-cause review |
Actual material availability, printing route, sample timing, minimum order quantity, test plan, acceptance criteria and production lead time remain subject to the final specification and written confirmation. For a wider supplier review, start with our drawstring bag manufacturer selection guide. Procurement teams building a broader sourcing policy can then consult the custom bag manufacturing pillar.
RFQ Checklist for Print Durability
Send the following information when requesting a quotation or sample:
| RFQ field | Information to provide |
|---|---|
| Bag | Material, construction, size, color, coating/finish and quantity |
| Artwork | Vector file, colors, dimensions, placement and coverage |
| Decoration | Preferred method or request for recommendation |
| Use | Event giveaway, retail packaging, gym, sports, product protection or other scenario |
| Contact risks | Folding, stacking, moisture, washing, repeated carry, rough contents or cleaning |
| Required methods | ISO/AATCC/ASTM/customer method and exact edition where specified |
| Acceptance | Grades, visual limits, cycle count, endpoint and approved reference |
| Sampling | Development sample, pre-production approval, test replicates and retention sample |
| Documentation | Photos, internal inspection record or qualified third-party report |
| Delivery | Destination, required arrival date, packaging and trade term |
This information can be incorporated into a complete specification using How to Prepare a Custom Drawstring Bag Tech Pack.
Frequently Asked Questions
Is a tape pull enough to approve a drawstring bag print?
No. A tape pull can screen for certain adhesion weaknesses, but it does not measure wet/dry color transfer, long-term abrasion, flex cracking, washing durability, or complete-bag wear. The tape and procedure must also be controlled if results will be compared.
Can ASTM D3359 be used directly on textile bags?
Not automatically. ASTM D3359-23 states that it was developed for coating films on metallic substrates and has scope limitations. A buyer may create a documented internal tape screen for a textile print, but should not label it ASTM D3359 compliance unless the method is applicable and actually followed.
What is the difference between crocking and abrasion?
Crocking evaluates color transferred by rubbing, commonly to a specified cloth. Abrasion examines physical surface wear. A specimen can show staining with little visible wear, or visible wear with limited color transfer.
Should dry and wet rubbing both be tested?
Test both when moisture exposure is reasonably expected or the buyer's specification requires it. The wet procedure must define moisture preparation and evaluation; an uncontrolled damp-cloth rub is not comparable to a recognized method.
How many abrasion cycles should a custom bag pass?
There is no universal cycle count for all drawstring bags. The number depends on apparatus, abradant, force, material, decoration, end use and agreed endpoint. A cycle count without these conditions is not meaningful.
Does passing a fabric abrasion test prove the printed logo will last?
No. A base-fabric abrasion result may say little about the bond or wear of an applied graphic. The decorated production-intent system and, when relevant, the finished bag should be evaluated.
When should washing be included?
Include washing when the care claim or intended use includes washing. Specify the complete washing and drying route, cycles and post-wash criteria. Do not describe a bag as machine washable based only on a rub test.
Why test an approved sample and a first production article?
The approved sample establishes the target; the first article confirms that production materials and settings reproduce it. Passing a development sample alone does not demonstrate run-to-run consistency.
What photographs should be retained?
Keep before-and-after views at consistent distance, angle and lighting, plus close-ups of tested areas and any removed material or stained rubbing cloth. Include the sample ID and test record outside the image rather than placing unverified claims inside it.
Can LUCKYSTAR guarantee a permanent print?
“Permanent” is not a responsible universal claim. LUCKYSTAR can help define the material, decoration, sample and test requirements, then coordinate evaluation against the written order specification. Final performance depends on the confirmed construction, method, use and acceptance criteria.
Final Buyer Takeaway
A reliable drawstring bag print test plan answers three separate questions: Will the decoration stay bonded? Will color transfer? Will repeated contact make the graphic unacceptable? It then connects those questions to a clearly identified specimen, controlled method, agreed endpoint and traceable report.
Before placing a bulk order, provide your bag material, artwork, intended use, care expectations and required test method. LUCKYSTAR can review the specification, recommend a production-intent sample route and confirm available testing and documentation options for the individual project.
Request a custom drawstring bag quotation and include your artwork, substrate, quantity, target market, handling conditions and print-durability requirements. All materials, methods, commercial terms and test commitments are subject to specification review and written confirmation.
Technical References
- International Organization for Standardization. ISO 105-X12:2016 — Textiles: Tests for colour fastness, Part X12: Colour fastness to rubbing. Current status checked September 28, 2026.
- American Association of Textile Chemists and Colorists. AATCC test-method directory, including TM8, Colorfastness to Crocking: Crockmeter. Checked September 28, 2026.
- ASTM International. ASTM D3359-23 — Standard Test Methods for Rating Adhesion by Tape Test. Scope limitations reviewed September 28, 2026.
- International Organization for Standardization. ISO 5470-1:2016 — Rubber- or plastics-coated fabrics: Determination of abrasion resistance, Part 1: Taber abrader. Status checked September 28, 2026.
- ASTM International. ASTM D4966-22(2026) — Abrasion Resistance of Textile Fabrics, Martindale Method. Status and cautions checked September 28, 2026.
- ASTM International. ASTM D5264-98(2019) — Abrasion Resistance of Printed Materials by the Sutherland Rub Tester. Scope checked September 28, 2026.
- International Organization for Standardization. ISO 6330:2021 — Domestic washing and drying procedures for textile testing. Status checked September 28, 2026.